English
 中文简体
 Español
How Can Kettle Base Connectors Simplify Component Inspection
Component inspection gets a lot easier when individual parts can be identified, accessed, and checked without creating unnecessary work across the production line. Nobody wants a quality worker dismantling half a base just to glance at one small piece tucked inside.
In electric kettle assembly, the base contains several connected parts, and the Kettle Base Connector can genuinely influence how easily those parts get separated and inspected during manufacturing. A connector may look like a small component sitting off to the side, but its position and connection method can affect disassembly, visual checking, component identification, and later assembly steps down the line.
For quality teams, this makes connector design relevant not only to product assembly but also to how inspection work actually gets organized on the floor. The relationship becomes a lot clearer when a Thermostat Connector, Thermostat Coupler, and Electric Kettle Base Coupler get treated as parts of the same inspection process, rather than as isolated components checked one after another.
A production team needs to know what each part is, where it belongs, how it connects with nearby components, and whether it can be checked without disturbing unrelated parts sitting close by. This creates a genuinely practical link between component design and quality management worth thinking through early in development.
Why Does Component Accessibility Matter During Kettle Inspection?
Inspection becomes a lot more complicated when a component is hard to reach or identify inside an assembled base. A quality worker may need to separate surrounding parts before checking a connector at all, which can add handling steps and create more opportunities for assembly errors to creep in.
An accessible component lets inspectors examine its visible condition and connection area with a lot less disruption to the surrounding structure. This proves particularly useful when inspection happens at several points during production, rather than only after the kettle has already been fully assembled and boxed.
| Inspection Need | Accessibility Consideration |
|---|---|
| Visual checking | Component should be reasonably visible |
| Part identification | Shape and position should be recognizable |
| Disassembly | Connection should be accessible |
| Reassembly | Parts should return to their intended positions |
| Quality records | Component identity should be easy to confirm |
The physical arrangement of the base can therefore affect how much effort inspection actually takes at each stage. A Kettle Base Connector placed in a genuinely crowded area may require a lot more handling than a similar component positioned with clearer access nearby.
This doesn't mean every connector needs to stay exposed during normal product use once the kettle leaves the factory. Instead, manufacturers can think carefully about how the component will actually get reached during controlled production inspection and maintenance activities.
How Can Disassembly Make Component Inspection Easier?
Disassembly gives quality teams a genuine way to inspect individual parts, rather than judging a complete base from the outside and hoping nothing's wrong underneath. The process becomes a lot smoother when components can be separated in a clear order without forcing workers to remove unrelated parts just to reach one piece.
A sensible disassembly arrangement can also make it a lot easier to pinpoint where a problem actually originates. For example, if a base contains a Thermostat Connector and several nearby components, inspectors need to distinguish the connector from the surrounding parts before checking its condition properly.
A clear component relationship supports this process considerably.
| Disassembly Stage | Inspection Purpose |
|---|---|
| Outer base access | Opens the inspection area |
| Connector separation | Exposes the connection point |
| Component identification | Confirms the part being checked |
| Individual inspection | Allows closer observation |
| Reassembly check | Confirms correct component placement |
The objective here isn't making every product easy to take apart for consumers at home. Factory inspection has genuinely different requirements, since trained workers are checking controlled production units, rather than carrying out everyday product repairs on a used appliance.
Manufacturers can therefore treat inspection access as part of production planning from the start. If a component repeatedly needs complicated handling before it can be checked at all, the production team may need to review its position, connection method, or surrounding assembly arrangement.
What Can a Thermostat Connector Reveal During Inspection?
A Thermostat Connector can provide genuinely useful inspection points, since its condition ties directly to how the surrounding base components get assembled together. Inspectors may need to confirm the connector is correctly positioned, properly attached, and free from visible damage before the product moves further along the line.
The inspection doesn't need to rest on one single observation made in passing. A quality check can consider the component itself, its connection with nearby parts, and its position within the base as a whole.
| Inspection Area | What Can Be Checked |
|---|---|
| Connector body | Visible condition |
| Connection area | Attachment condition |
| Position | Correct placement |
| Nearby components | Possible interference |
| Assembly area | Signs of incorrect installation |
Component identification also matters a great deal when several parts share similar shapes sitting nearby. A connector that resembles another component may get misidentified, if workers rely only on appearance without checking further.
Clear production documentation and organized component storage help cut down this confusion considerably. The physical design of the Thermostat Connector can also support recognition, when its shape, position, and connection relationship stay consistent across the whole production run.
This gives inspection teams a genuinely clearer reference point when checking assembled kettle bases one after another on the line.
How Does a Thermostat Coupler Support Quality Checks?
The Thermostat Coupler can get viewed from the same inspection angle, particularly when it connects components that need separating during production checks. A coupler that's easy to identify and access without unnecessary interference can make inspection work a lot simpler to organize across a shift.
Quality management often involves repeated checks across different production stages, so small handling differences can become genuinely significant once they occur throughout a manufacturing workflow day after day. Inspectors may need to confirm the coupler is present, correctly positioned, properly connected, and free of visible damage before the next assembly stage kicks off.
The surrounding component layout influences quite a bit how smoothly these checks actually get performed on the floor.
If the coupler sits hidden behind several unrelated parts, workers may need extra time opening the assembly before even reaching it. If the inspection area is more accessible instead, the same check may fit a lot more naturally into the production sequence without slowing anything down.
| Thermostat Coupler Check | Production Question |
|---|---|
| Component identity | Is the intended part being inspected? |
| Position | Is it located correctly? |
| Connection | Is it attached as required? |
| Surrounding space | Can nearby parts interfere? |
| Reassembly | Can the component return correctly? |
The purpose behind this approach isn't piling on unnecessary inspection work onto an already busy line. It's making existing quality checks a lot easier to perform and easier to repeat consistently, shift after shift.
A manufacturing team can then build inspection points around the actual structure of the kettle base, rather than inventing separate procedures for every small component tucked inside it.
Why Is Component Identification Important in Production Inspection?
Component identification becomes particularly important when a kettle base holds several parts with related functions or genuinely similar appearances at a glance. An inspector needs to know exactly which component is being checked before recording an inspection result on paper.
Clear identification cuts down the chance of checking the wrong part entirely or returning a component to the wrong position after disassembly wraps up. Manufacturers can support identification through consistent component shapes, organized workstations, clear assembly documentation, and logical component placement across the line.
These methods work together as a system, rather than leaning on one identification feature to carry the whole load.
A Kettle Base Connector may be a lot easier to recognize when its position within the base stays consistent from one unit to the next on the line. The same principle applies just as well to a Thermostat Connector and Electric Kettle Base Coupler sitting nearby.
When the production team knows exactly where each component belongs, inspection becomes genuinely easier to structure from the outset.
| Identification Method | Practical Use |
|---|---|
| Component shape | Helps visual recognition |
| Assembly position | Shows where the part belongs |
| Connection relationship | Distinguishes related components |
| Production documentation | Supports worker reference |
| Organized storage | Reduces component confusion |
This can also help quite a bit during reassembly afterward. Once inspection wraps up, components need to return to their intended locations, and clear identification makes that task a lot easier to control consistently.
For quality management, inspection and reassembly should therefore get treated as one connected process, not two separate steps. A component that's easy to inspect but hard to identify during reassembly can still create unnecessary production risks further down the line.
How Can Connector Placement Affect Inspection Workflow?
Connector placement influences quite a bit how inspectors actually approach the base once it lands on their bench. A component positioned near an accessible inspection area may get checked without disturbing other parts nearby, while a connector buried deep inside the assembly may need additional disassembly first.
This can affect the order in which quality checks actually get performed across a shift. Manufacturers can weigh carefully whether frequently inspected components should sit where workers can reach them without unnecessary handling each time.
The arrangement can also shape how the production line itself gets organized around it.
| Placement Situation | Possible Inspection Effect |
|---|---|
| Accessible connector area | Easier visual checking |
| Crowded component area | More difficult handling |
| Clear separation between parts | Easier identification |
| Overlapping assembly areas | More complicated disassembly |
| Consistent component position | Simpler inspection routine |
Connector placement still needs to fit the product's overall structure, of course. A manufacturer cannot move every component solely for inspection convenience, since the base must also accommodate other parts and assembly requirements that matter just as much.
The genuinely useful approach is weighing inspection alongside assembly right when the base layout gets developed, not bolted on as an afterthought later. This can help production teams spot areas where a small design tweak could make inspection a lot more manageable without changing the basic function of the product at all.
What Inspection Issues Can Appear During Disassembly and Reassembly?
Disassembly opens access to individual components, sure, but it also introduces another quality concern worth watching for. Every time a part gets separated and returned to its position, there's a genuine possibility of incorrect placement, incomplete connection, or damage caused by careless handling along the way.
This is why inspection procedures need to think through carefully what happens after the component has already been checked once. A Electric Kettle Base Coupler may look visually fine before disassembly starts, but the production team still needs to confirm its condition after it's been handled and returned to the assembly afterward.
The same holds just as well for the Thermostat Coupler and other base components sitting nearby.
Quality checks can therefore get divided around the inspection process as a whole.
| Production Point | Quality Focus |
|---|---|
| Before disassembly | Original component condition |
| During separation | Component and connection condition |
| Individual inspection | Visible part condition |
| During reassembly | Correct component placement |
| After reassembly | Overall assembly condition |
This approach helps prevent inspection from turning into a genuinely one-sided activity focused only on the easy part. A component may pass an individual visual check just fine but still create an assembly issue, if it gets returned incorrectly afterward.
Production teams can cut this risk down by making the disassembly and reassembly sequence genuinely clear to the workers responsible for inspection each day. The simpler the relationship between component identity, position, and connection stays, the easier it becomes to hold a consistent workflow together across shifts.
How Can Manufacturers Build Inspection Into Kettle Base Production?
Quality inspection is a lot easier to manage when it gets factored in during product development, rather than tacked on after assembly procedures have already been locked in place. Manufacturers can review the base structure early and figure out which components need regular checking, where inspectors need genuine access, and how parts will get handled during inspection.
The Kettle Base Connector can get weighed within this broader layout from the start. Its position, connection method, surrounding components, and accessibility can all shape the inspection process considerably.
A practical development review can work through several questions worth asking early on. Can inspectors identify the component without confusion creeping in? Can the inspection area be reached without unnecessary disassembly slowing things down? Can nearby components stay undisturbed during the check itself? Can the part be returned to its intended position after inspection wraps up? Can workers follow the same inspection sequence consistently across production units?
These questions connect product design with factory quality management in a genuinely practical way. They also help manufacturers tell apart an assembly issue from a plain inspection-access issue that looks similar at first glance.
A Thermostat Connector that's difficult to inspect may not actually have a problem with its basic function at all, but its position could still make production checks a lot harder to perform consistently across a shift. The same principle can apply just as well to an Electric Kettle Base Coupler, when its location forces several surrounding components to get removed before inspection can even start.
A more inspection-friendly arrangement can cut down unnecessary handling considerably and make component checks a lot easier to weave into the production workflow as a whole. This perspective proves genuinely useful for both product engineers and quality teams, since it treats inspection as part of manufacturing itself, rather than as an activity that only happens once the product's already fully assembled.
When connector identity, component position, disassembly access, inspection points, and reassembly all get weighed together, the kettle base becomes a lot easier to manage throughout production from start to finish.
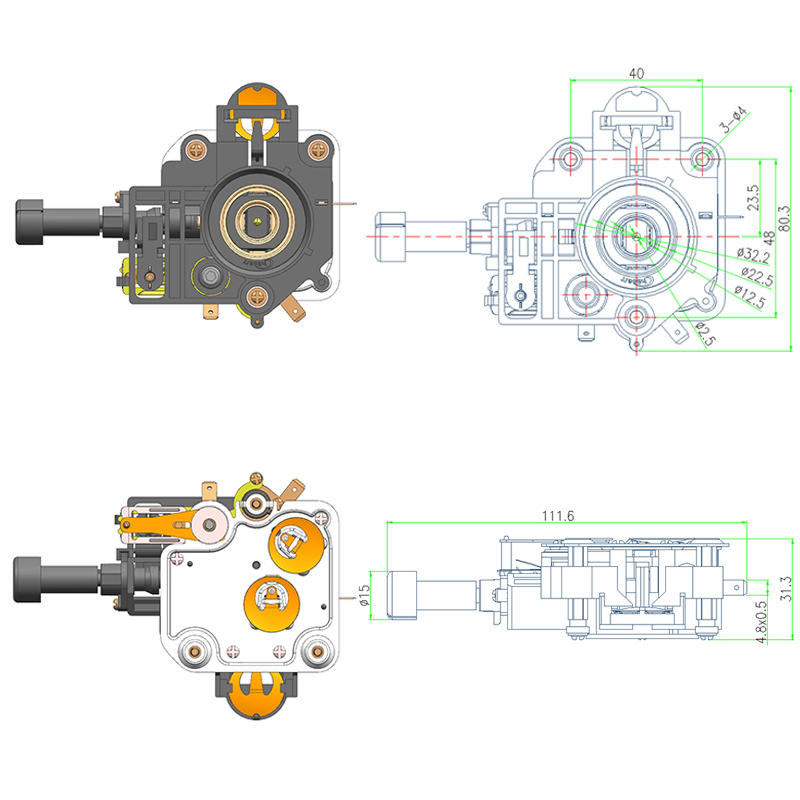
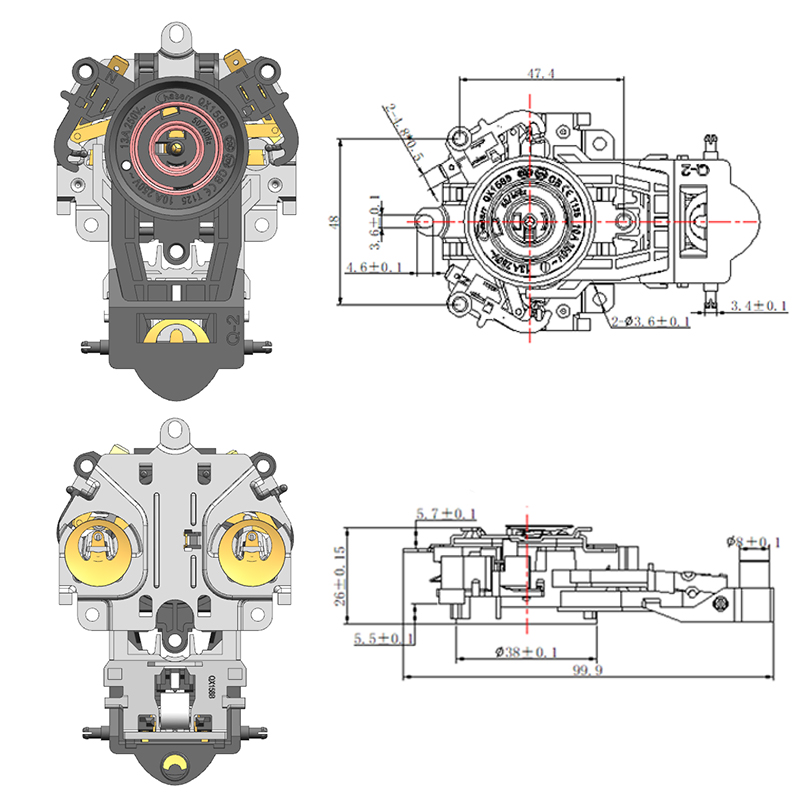
That connection also gives manufacturers a genuinely practical way to review the role of the Thermostat Coupler, Thermostat Connector, Kettle Base Connector, and Electric Kettle Base Coupler within the actual inspection process, instead of evaluating each component in isolation without considering its place in the finished assembly.
Featured Products

-
No. 2892, Ningkang East Road, Tiancheng Industrial Zone, Yueqing City, Zhejiang Province
-
 Email: Una@chaserr.cc
-
 Phone: +86-13075775533
- GET IN TOUCH

Electric Kettle Thermostat Coupler Manufacturer